
أخبار الصناعة
Edge Banding Troubleshooting: Why Panels Peel, Gap, or Show Glue Lines
Edge Banding Troubleshooting should start with the defect you see on the panel, not with random machine adjustment. If panels peel, leave gaps, show glue lines, or trim unevenly, the cause is usually hidden in glue temperature, pressure roller setting, panel edge preparation, feed speed, trimming adjustment, or maintenance. This guide helps operators find the likely cause, test it quickly, and stop wasting boards.
جدول المحتويات
Why Should Edge Banding Troubleshooting Start with the Symptom?
Edge Banding Troubleshooting becomes faster when the operator asks one question first: where does the defect appear?
A bonding failure points to glue, pressure, tape, or board condition. A gap may come from the panel edge, guide rail, or pressure roller alignment. A trimming defect may have nothing to do with glue at all.
Use this first check before changing settings:
| Symptom | First Area to Check |
|---|---|
| Tape not sticking | Glue temperature, glue pot, pressure rollers |
| Gaps between tape and board | Panel edge, guide rail, pressure contact |
| Peeling after trimming | Blade sharpness, bonding strength, cooling time |
| Visible glue line | Glue amount, scraper, tape color match |
| Uneven trimming | Cutter, copy wheel, air pressure |
ال H.B. Fuller hot melt guide explains that hot melt adhesive open time must match the application; if it is too short, the substrate may not wet out and bonding may fail. That is why Edge Banding Troubleshooting should always connect glue behavior with machine speed and pressure.
Why Is the Edge Banding Not Sticking?
This is the most common problem in any Edge Banding Troubleshooting job. Poor bonding often comes from low glue temperature, old glue, dusty panel edges, moisture, weak pressure roller force, fast feed speed, or unsuitable edge tape.
ال Applied Adhesives guide to successful hot-melt bonding highlights factors such as temperature, open time, set time, and substrate placement. In edge banding, those factors decide whether glue can wet the panel edge before pressure is applied.
Quick checks:
- confirm glue pot and roller temperature;
- clean the glue roller and applicator;
- check whether glue spreads evenly;
- inspect pressure roller contact;
- remove dust from the panel edge;
- test another tape and glue batch.
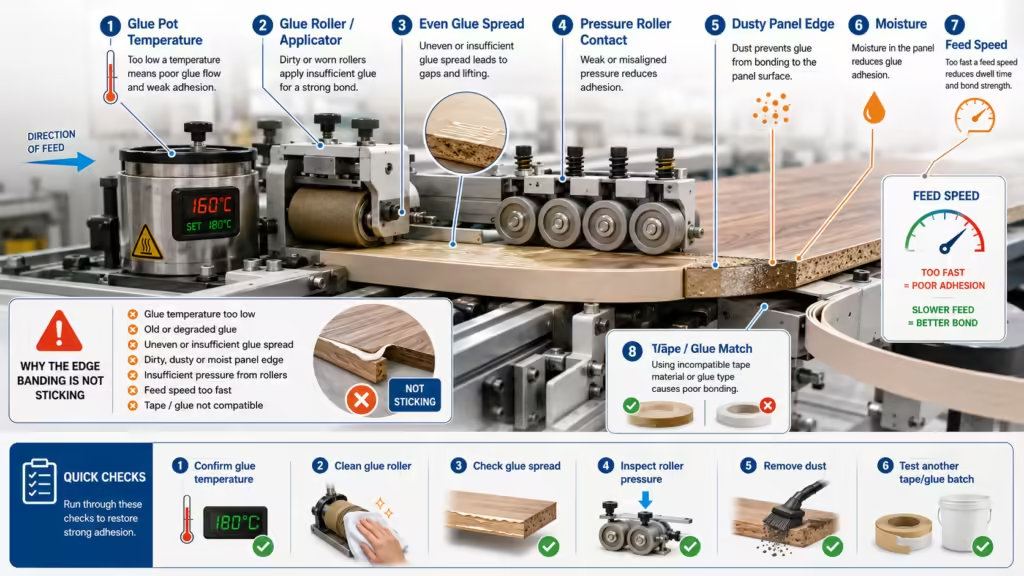
If poor bonding is the main issue, this detailed guide on edge banding not sticking causes and fixes can help you check glue temperature, pressure, material condition, and machine settings more deeply.
Why Is the Edge Banding Machine Leaving Gaps?
Edge Banding Troubleshooting for gaps should not blame glue too early. If the tape sticks in some areas but leaves open lines in others, first inspect panel preparation and pressure alignment.
تشمل الأسباب الشائعة ما يلي:
- panel edge not straight after cutting;
- pre-milling not removing chips;
- guide rail not aligned;
- pressure roller not contacting evenly;
- tape width or thickness mismatch;
- insufficient glue spread;
- feed speed too high.
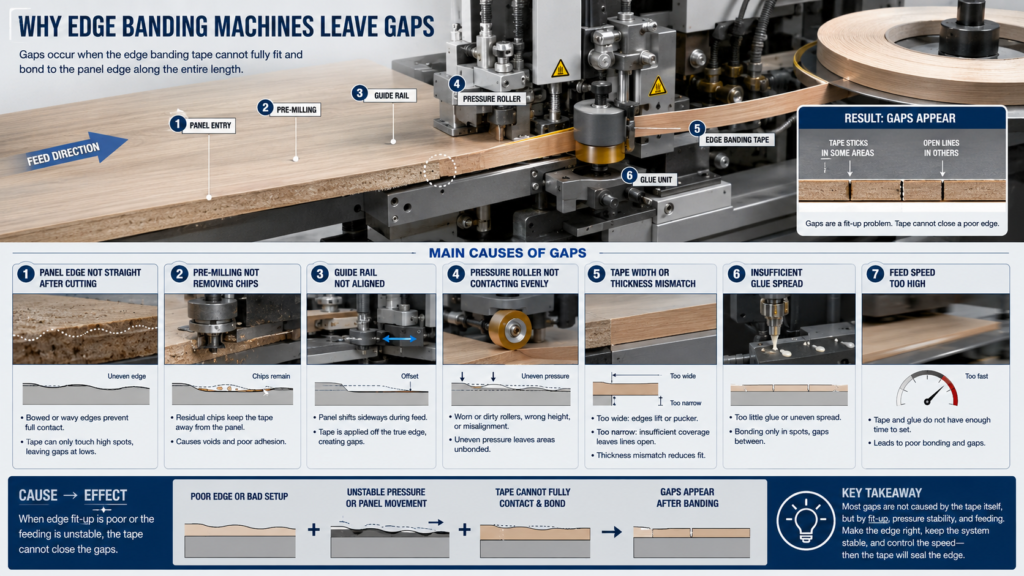
A gap is often a fit-up problem. The tape cannot close a poor edge if the board is not square, the pressure unit is not stable, or the panel moves during feeding.
Why Does Edge Banding Peel Off After Trimming?
This Edge Banding Troubleshooting step is different from ordinary bonding failure. Sometimes the tape looks fine after pressing, then lifts after trimming, end cutting, or corner rounding.
تحقق من هذه النقاط:
1.Is the trimming blade dull?
2.Is the cutter removing too much tape?
3.Is the end-cutting impact too strong?
4.Has the glue cooled enough?
5.Is the tape supported during trimming?
6.Is the bonding already weak before trimming?
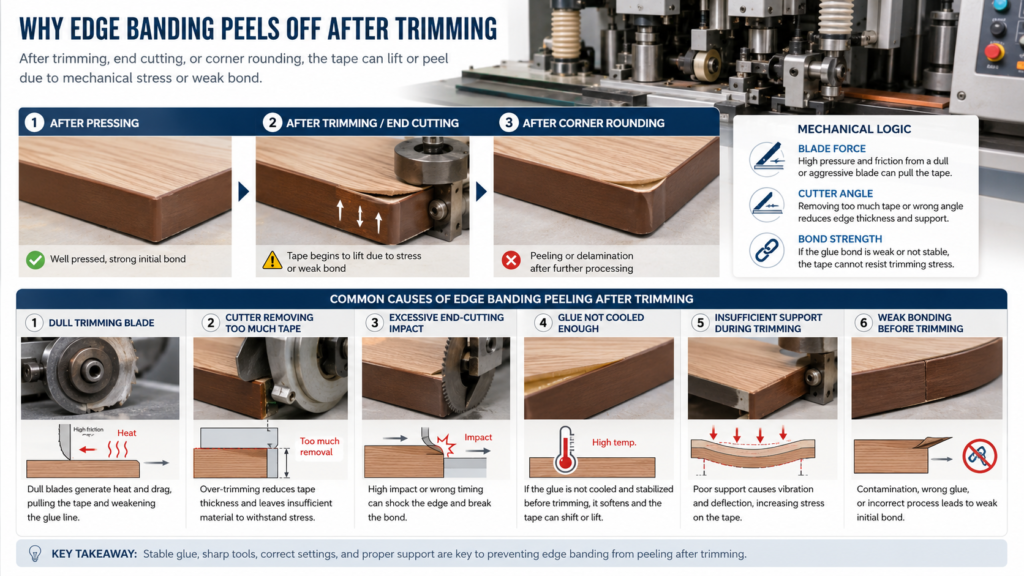
If peeling starts only after trimming, the issue may be blade force, cutter angle, or weak bonding strength. Replacing a worn blade may solve what looks like a glue problem.
Why Are Glue Lines Too Thick or Too Visible?
Visible glue lines are a common Edge Banding Troubleshooting complaint in furniture factories, especially on white panels, light woodgrain boards, and high-gloss surfaces.
A thick or colored glue line may come from too much glue, wrong glue color, high glue temperature, low pressure, an uneven board edge, or poor scraping and buffing adjustment.
| Defect | السبب المحتمل |
|---|---|
| Thick glue bead | Too much glue or low pressure |
| Yellow glue line | Glue color mismatch |
| Glue overflow | Excess glue or high temperature |
| Dirty edge after buffing | Scraper or buffing wheel issue |
ال SURTECO edgeband troubleshooting page lists practical causes such as too little pressure, cold adhesive, and board or edgebanding temperature problems. This is the one industry reference in this article because it directly addresses edgebanding behavior.
Why Are Trimming, Scraping, or Buffing Results Uneven?
Edge Banding Troubleshooting should also cover finishing units. Not every defect comes from the glue station.
Uneven finishing may show as tape not flush with the panel, over-trimming, remaining glue residue, scraping white lines, rough corners, or inconsistent radius.
Check:
- trimming blade sharpness;
- cutter angle and depth;
- copy wheel pressure;
- panel thickness variation;
- air pressure stability;
- scraper position;
- buffing wheel wear and contact.
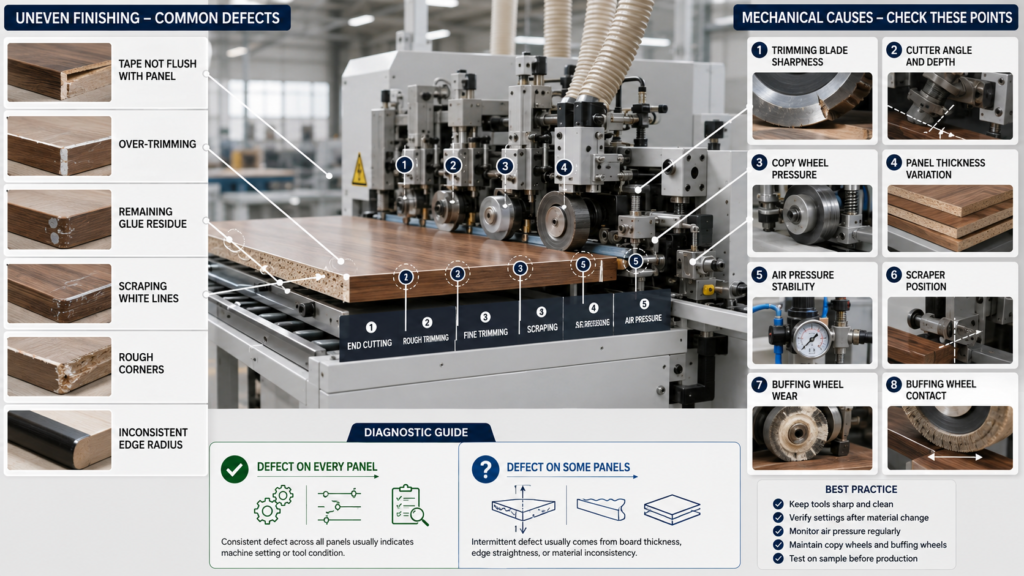
If the same defect appears on every panel, inspect the machine setting. If it appears only on some panels, check board thickness, edge straightness, and material consistency.
Quick Machine Repair Guide for Edge Banding Troubleshooting Before You Stop Production
A practical machine repair guide should follow a fixed order, because Edge Banding Troubleshooting needs repeatable checks, not guesswork. The HSE safe use of woodworking machinery guidance covers training, information, and guarding for woodworking machinery, while the SafeWork NSW edge bander hazard identification page focuses on edge bander risk management.
For safe Edge Banding Troubleshooting, isolate unsafe energy sources before opening guarded areas or touching moving parts.
| Machine Area | What to Check |
|---|---|
| Glue pot | Temperature, glue quality, clogging |
| Glue roller | Amount and even spread |
| Pressure rollers | Pressure, alignment, wear |
| Feed system | Speed, guide rail, panel stability |
| Trimming unit | Blade, depth, angle |
| Scraping unit | Pressure and edge finish |
| Buffing unit | Wheel wear and contact |
| Air system | Stable pressure and cylinder action |
When Should Operators Stop Adjusting and Call for Service?
Edge Banding Troubleshooting should stop when adjustment becomes guessing. Call for service if glue temperature fluctuates, pressure rollers wobble, motors sound abnormal, air cylinders respond slowly, alarms repeat, or panels keep failing after several test runs.
The CCOHS machinery safety guide notes that machine guarding helps prevent contact with hazardous moving parts. If troubleshooting requires access behind guards, follow proper lockout and maintenance procedures.
How Can Factories Prevent the Same Problems?
Edge Banding Troubleshooting is cheaper when it becomes daily prevention. Clean the glue pot, check roller pressure, sharpen blades, inspect air pressure, test scrap panels, record glue settings, and keep board edges straight and dust-free.
Run one test panel before mass production. Treat Edge Banding Troubleshooting as a production habit, not an emergency task. It is better to reject one test piece than to waste a full batch.
التعليمات
Why is my edge banding machine not sticking?
Usually because of low glue temperature, poor glue quality, dusty panel edges, weak roller pressure, fast feed speed, or unsuitable edge tape.
Why is my edge banding machine leaving gaps?
Gaps often come from uneven panel edges, poor guide rail alignment, wrong tape size, weak pressure contact, or insufficient glue spread.
Why does edge banding peel off after trimming?
The bond may be weak, the trimming blade may be dull, the cutter may remove too much material, or the glue may not have cooled enough.
How do I fix visible glue lines?
Check glue amount, temperature, pressure roller setting, tape color match, scraper position, and buffing performance.
Why is the edge tape not flush with the panel?
The trimming unit may be misadjusted, the blade may be worn, the copy wheel pressure may be wrong, or panel thickness may vary.
When should I call a technician?
Call a technician if alarms repeat, motors sound abnormal, air cylinders act slowly, temperature control fails, or repeated Edge Banding Troubleshooting does not stop panel waste.